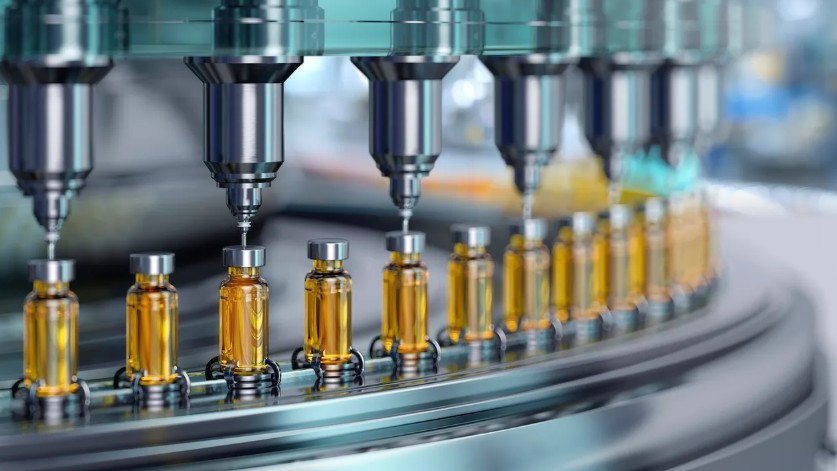
Pharmaceutical and medical device manufacturers are bringing sustainability, artificial intelligence, and facility optimization together as part of a broader shift in production strategy. Owen Bonner, COO of Honeywell Technologies Life Sciences, explains that these priorities are increasingly connected to reliability, resilience, and competitiveness rather than treated as separate initiatives, tells Design News.
Sustainability now extends beyond reducing carbon emissions. Manufacturers must manage energy, solvents, equipment, and other resources while maintaining dependable production. This is especially important for high-demand products such as GLP-1 drugs, which can require substantial quantities of solvents. Better resource management can therefore support both environmental goals and operational continuity.
AI is also moving from experimentation into regulated manufacturing workflows. Honeywell uses AI within quality management systems for tasks such as transcribing, translating, classifying, and analyzing customer complaints. Human oversight remains essential. When an AI system cannot complete a task reliably, the work is escalated to a person. Bonner says AI systems are achieving reliability in the high 90% range for some applications, but governance, validation, and supervision remain necessary.
AI is also helping manufacturers execute projects faster. Honeywell reports that its tools can reduce time to value by 50–60% for certain tasks, with AI performing initial work before experts complete the process.
Facility design presents another opportunity. Rather than relying solely on new factories, manufacturers can increase capacity within existing sites. Modular plants designed for easier modification can accelerate the addition of products and production lines while reducing disruptive changes.
Greenfield and brownfield projects present different challenges. New facilities can incorporate newer technology but require recruiting and training workers. Digital twins can begin training employees before construction is complete. Existing facilities already have experienced personnel but need flexible systems that simplify upgrades.
Together, AI, digital twins, modular design, and resource efficiency are changing pharmaceutical manufacturing into a more adaptable model focused on expanding capacity while maintaining safety and regulatory control.
